GET 100 CUT-OFF WHEELS IN A BONUS TOOLBOX

Mounted flap wheels

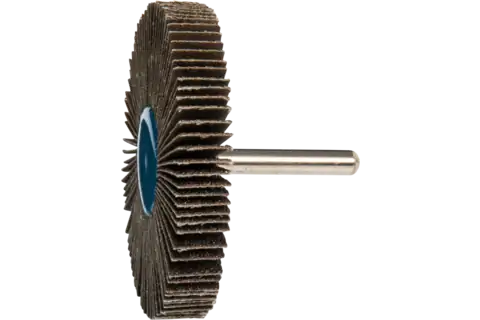
Mounted Flap Wheel, 3″ x 1/2, 80 Grit, 1/4″ Shank, Silicon carbide

EDP:
45438
Technical data Change variant

Login / Register
Choose options
Abrasive
Dia. external
Dia. shank
Grit size
Width
Packaging unit
Technical information
Mounted Flap Wheel, 3″ x 1/2, 80 Grit, 1/4″ Shank, Silicon carbide

Item number Global part number
47800181
Abrasive
Silicon carbide SiC
Dia. external
3 Inch
Dia. shank
1/4 Inch
Dia. shank
6.35 mm
EDP no.
45438
Grit size
80
Length, shank
1-1/2 Inch
Max. RPM
20000 RPM
RPM, optimum
4800 RPM
Width
1/2 Inch
Packaging unit
10 pieces
Description

With mounted flap wheels, coated abrasive flaps are arranged radially around the core in a fan-like structure. The flexible flaps perfectly adapt to surface contours. The abrasive grain is embedded in the sturdy, flexible cloth backing material with a resinoid bond.

In ISO 3919, mounted flap wheels are designated as "flap wheels with shaft."

For universal grinding work on components made from aluminium, copper, bronze, titanium and fibre-reinforced plastics. Excellent for use on titanium alloys. Ideal for the aeronautical industry, especially where SiC is the only approved abrasive, e.g. for use on engine components.

Special features
  • Conforms to contours due to high flexibility.
  • Consistently high stock removal rate throughout the entire service life as new, aggressive abrasive is constantly exposed.
  • Can be used face-down very close to edges and in corners due to the flat, molded-core design.
Recommendations for use
  • Flap wheel wear and the thermal load on the workpiece are reduced by decreasing the contact pressure and peripheral speed, and by adding grinding oil.
  • Stock removal rate should be increased by using a coarser grit, not by increasing the contact pressure. This avoids unnecessary flap wheel wear and prevents the thermal load of the workpiece.
  • Increasing the speed results in a slightly finer surface quality. An increase in contact pressure results in a slightly coarser surface. The softer the workpiece material, the coarser the resulting surface (when using the same grit size).
  • For the best performance, use with a recommended peripheral speed of 3,000-4,000 SFPM. This provides an ideal compromise between stock removal rate, surface quality, thermal load on the workpiece and tool wear.
  • Use the appropriate grinding oil for the material to significantly increase the service life and the abrasive performance of the discs.
Safety notes
  • For safety reasons, the maximum permitted rotational speed indicated must never be exceeded.
  • The contact pressure has to be reduced significantly when the optimum rotational speed is exceeded.
  • Ensure the clamping depth is at least 5/8" and the specified maximum rotational speed is not exceeded with unsupported shank lengths.
Workpiece materials
Aluminum
Bronze
Fibre-reinforced thermosetting plastics (GRP, CRP)
Stainless steel (INOX)
Stone
Thermoplastics
Titanium
Titanium alloys
Applications
Deburring
Leveling
Step-by-step fine grinding
Structuring (matt finishing, brush matting and satin finishing)
Surface work
Work on weld seams
Compatible power tools
Flexible shaft drive
Straight grinder
Downloads